Technical Resources
How Cosmetic Defects Are Inspected on Optical Components
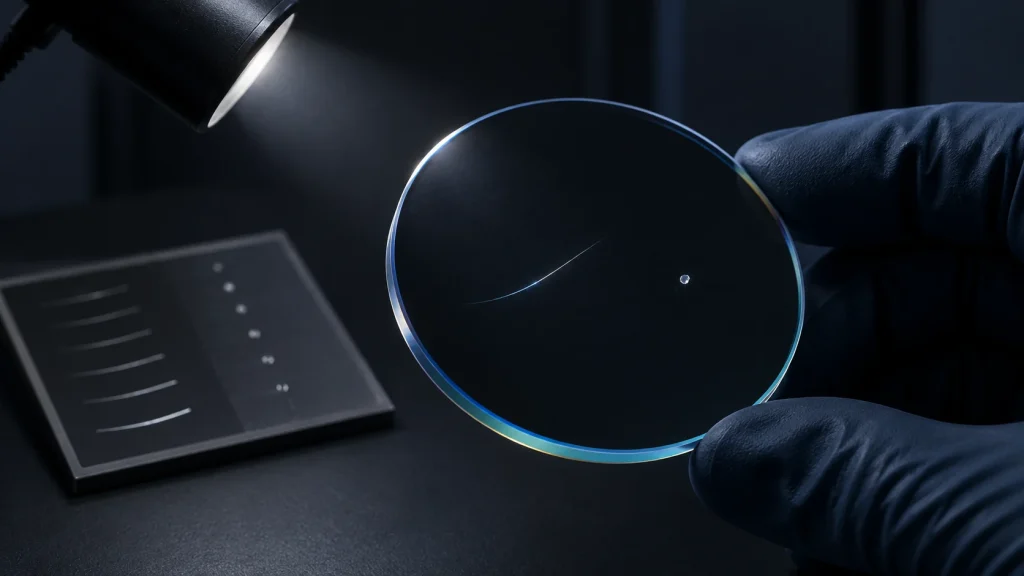
Cosmetic defects on optical components — scratches, digs, edge chips and coating blemishes — are inspected by cleaning the part, viewing each surface inside its clear aperture under controlled dark-field lighting against a black background, and then grading what is seen in the way the drawing specifies: by comparing scratch brightness with calibrated standards (visibility method) or by measuring defect size under magnification (dimensional method). The result is accepted or rejected only against the stated callout, such as MIL-PRF-13830B, ISO 10110-7 or ANSI/OEOSC OP1.002.
The physics behind every visual method is the same. A polished surface reflects or transmits light specularly; a scratch, pit or coating void scatters it. Against a dark field, that scattered light makes a sub-micron feature visible to the eye even when it is far below the eye’s resolving limit. This is why lighting geometry, background and viewing angle matter as much as the inspector — and why two inspections of the same lens can disagree when those conditions are not controlled.
What counts as a cosmetic defect on an optical surface
“Cosmetic” refers to localized surface imperfections, not to surface form or roughness. Flatness and irregularity are measured interferometrically, and microroughness by profilometry or scatter; neither is judged by a scratch-dig inspection (see scratch-dig vs surface roughness and surface flatness vs wavefront error). The defect families below are the ones a cosmetic inspection is designed to find.
| Defect | What it is | How it is typically specified | Best way to see it |
|---|---|---|---|
| Scratch | Elongated mark from grinding, polishing or handling | Visibility number (MIL-style, e.g. 40) or width/area grade (ISO 10110-7 dimensional) | Dark-field reflection; rotate the part so the scratch lies across the light |
| Sleek | Fine polishing scratch with smooth edges, often hard to see | Treated as a scratch | Dark-field at varied angles; high-magnification microscopy (e.g. DIC) when sizing is required |
| Dig / pit | Small crater or pit left in the surface | Dig number = diameter in 0.01 mm (MIL); square-root-of-area grade (ISO) | Dark-field; size with a reticle loupe or microscope |
| Bubble / inclusion | Bulk material imperfection, not a surface defect | Usually a material callout (e.g. ISO 10110-3), sometimes counted as digs by local practice | Transmitted light through the bulk |
| Edge chip | Material broken away at the edge or bevel | Maximum chip size from the edge (ISO “E” term or drawing note) | Grazing light along the edge; measure with a reticle |
| Coating defect | Pinhole, spatter, void, stain, blister or peeling in a thin film | ISO 10110-7 “C” term, ANSI OP1.002 coating terms or a project note | Reflection for spatter and stains; transmission against a bright source for pinholes in reflective or high-blocking coatings |
Start with the drawing: which standard and which method?
A cosmetic inspection can only be as objective as the callout it enforces. Before anyone picks up a lamp, the inspector needs four things from the drawing or specification: the standard, the method, the grade for each surface, and the zone it applies to — normally the clear aperture (see clear aperture vs optic diameter).
Visibility method (MIL-PRF-13830B style)
A callout such as 60-40 or 20-10 is a visibility specification. The first number is a scratch visibility grade, assigned by comparing the scratch side by side with a set of calibrated comparison scratches under the same lighting. It is not a width in microns: scratch visibility depends strongly on cross-section shape, so measuring a scratch’s width cannot establish its grade. The second number is the dig grade, which is dimensional — the dig diameter in hundredths of a millimetre, so dig 20 means 0.20 mm, with irregular digs taken as the average of length and width.
Because commercial comparison sets are not all equivalent to the original U.S. Army master, a robust drawing names the comparison standard used for acceptance. Supplier and customer should grade with equivalent sets, or results will drift.
Dimensional method (ISO 10110-7 style)
ISO 10110-7 describes imperfections by area rather than brightness. A callout written as 5/N×A allows N imperfections of grade A, where A is the square root of the imperfection area in millimetres. Additional terms can be added: L for long scratches (specified by width), E for edge chips and C for coating imperfections. Since the 2017 edition, ISO 10110-7 also offers a visibility notation in scratch-dig form, so an ISO drawing may carry either system — read the notation, not just the standard number.
ANSI/OEOSC OP1.002 provides both systems as well: a numerical visibility notation modeled on MIL-PRF-13830B and an alphabetical dimensional notation modeled on MIL-C-48497A and MIL-F-48616, and it also addresses edge, coating and cement imperfections. Drawings prepared under Chinese national practice may express surface imperfections as a GB/T 1185 grade; there is no exact one-to-one conversion between such grades and MIL scratch-dig numbers, so the acceptance standard should be agreed explicitly rather than “translated” by assumption.
How cosmetic defects are inspected: a step-by-step workflow
The sequence below reflects common industry practice for visual inspection of lenses, windows, filters, mirrors and prisms. The exact lighting and viewing conditions should follow the standard named on the drawing.
- Confirm the callout per surface. Note the standard, the method (visibility or dimensional), the grade for each surface, whether the requirement applies before or after coating, and the inspection zone. Surfaces often carry different grades — a laser-facing surface may be tighter than a rear surface.
- Handle and clean correctly. Hold the part by its edges with gloves or finger cots and clean it with the method approved for its coating (see methods for cleaning optical filter coatings). Dust, lint and residue scatter light just like defects. A gentle stream of clean, dry gas helps separate the two: anything that moves or changes after re-cleaning is contamination, not a dig.
- Set up the inspection station. A dark room or hood, a matte black background, and a defined light source at an oblique angle so the specular reflection does not enter the eye. MIL-PRF-13830B visual inspection, for example, is commonly performed with a 40 W incandescent or 15 W cool-white fluorescent lamp. Allow the eyes to adapt to the low ambient light.
- Scan the whole zone in reflection and in transmission. Tilt and rotate the part slowly. A scratch is most visible when it runs perpendicular to the plane of illumination, so a single fixed angle can miss it. Transparent parts are also viewed in transmitted light; mirrors and high-blocking coatings are checked against a bright source for pinholes.
- Classify and grade each indication. For visibility grading, compare the scratch with the comparison standard placed next to the part under identical lighting. For digs and dimensional grades, measure with a reticle loupe or a calibrated microscope.
- Apply the accumulation rules. A part does not pass just because each individual defect is within grade. The standards limit the number, combined length, total area and concentration of defects (see the worked example below).
- Record the result. Record surface, zone, standard, method, comparison set or instrument, and the accept/reject decision. If the drawing requires a report, its format should be agreed before production.
Lighting and viewing geometry: why it decides what you see
Dark-field viewing works because the eye sees only light scattered toward it. If the inspector looks into the specular reflection of the lamp, glare swamps the scatter and fine scratches disappear. If the lamp is too dim or the background is not black, low-visibility grades such as 10 or 20 cannot be judged at all. This is the main reason visual results vary between sites: different lamps, backgrounds, distances and comparison standards produce different apparent brightness for the same scratch.
Component geometry adds its own difficulties:
- Curved lenses produce shifting reflections; the part must be rotated through several orientations, and steep surfaces may need an adapted fixture.
- Coated optics can make polishing marks more visible than they were on the bare substrate, which is why the callout should state whether it applies after coating.
- Filters and mirrors with high reflectance or high optical density reveal pinholes best when viewed in transmission against a bright, uniform source. A cosmetic pass does not prove spectral performance; that is a separate measurement (see how to evaluate optical filter performance).
- Cemented components and prisms show defects at internal interfaces and faces through the bulk, so the viewing direction must be chosen surface by surface.
Visual inspection, microscopy and machine vision compared
ISO 14997 groups inspector-based test methods into two families. Visibility methods evaluate brightness with or without a comparison artefact; dimensional methods estimate size by eye, compare against an artefact of known size, or measure with magnification and a reticle or ruler. Fully instrumented approaches such as digital microscopy and scatterometry sit outside that standard, while ISO/TR 14997-2:2022 gives guidance on configuring machine vision to grade ISO 10110-7 callouts using dark-field principles.
| Method | What it determines | Strengths | Limitations |
|---|---|---|---|
| Visual comparison under dark-field lighting | Scratch visibility grade; presence of digs, chips and coating defects | Fast; covers the whole aperture; the reference method for visibility callouts | Subjective; depends on lighting, comparison set and inspector training |
| Reticle loupe | Dig diameter, chip size, approximate defect dimensions | Simple; adds a dimension to a visual finding | Limited resolution; cannot assign a visibility scratch grade |
| Calibrated microscope (bright-field, dark-field or DIC) | Defect size and area for dimensional grades; fine sleeks | Objective sizing; suits tight grades and small parts | Small field of view, so full-aperture coverage is slow and costly |
| Automated machine-vision system | Defect location, size and count across the surface | Repeatable; produces records; suited to volume inspection of flat parts | Must be calibrated and correlated with the drawing’s method; curved and coated parts need adapted illumination |
In practice the methods are combined: a full-aperture dark-field scan finds the indications, and magnification is used only on the ones that need sizing.
Applying the acceptance rules: two illustrative examples
Illustrative only. The examples below show how the rules are applied; they are not GIAI product specifications. Use the full text of the applicable standard for acceptance decisions, because each standard contains further summation and concentration rules not reproduced here.
MIL-PRF-13830B, 40-20 on a 25 mm diameter surface
- The largest permitted dig is 0.20 mm in diameter.
- Maximum-size digs are limited to one per 20 mm of diameter or fraction thereof: 25 ÷ 20 = 1.25, so two maximum-size digs are allowed on that surface.
- When maximum-visibility (grade 40) scratches are present, their combined length may not exceed one quarter of the diameter: 25 ÷ 4 = 6.25 mm.
- Further rules limit the total of all dig diameters and the combination of smaller scratches.
ISO 10110-7, 5/3×0.25
- Up to three imperfections of grade 0.25 are allowed, each with an area up to 0.25 × 0.25 = 0.0625 mm².
- The total area budget is 3 × 0.0625 = 0.1875 mm²; the standard allows smaller imperfections to be counted against this budget under defined rules.
- Long scratches, edge chips and coating imperfections are only limited if the L, E and C terms are present on the drawing.
Common mistakes that make inspection results disagree
- Grading a visibility scratch by measuring its width. Width and visibility are poorly correlated; a microscope reading does not convert to a scratch number.
- Using non-equivalent comparison standards at the supplier and at incoming inspection.
- Inspecting a dirty part and recording residue as digs, or over-cleaning and creating new sleeks.
- Not stating the inspection zone. Without a defined clear aperture, it is unclear whether a defect near the edge counts.
- Mixing up coated and uncoated states. A part that passes before coating may not pass after, or vice versa.
- Treating a cosmetic grade as a performance specification. Scratch-dig does not specify surface form, wavefront error, spectral performance or laser-induced damage threshold, although defects can increase scatter and act as damage initiation sites in laser optics.
- Over-specifying. Tighter grades require more polishing, handling care and inspection time. The grade should follow the defect’s real effect in the system: its position relative to an image plane or focus, the beam size, the laser power and the stray-light tolerance.
What to state on the drawing or RFQ so inspection is unambiguous
- Standard and edition, and the method — visibility or dimensional
- Grade for each surface, including any coating (C) and edge chip (E) limits
- Inspection zone: clear aperture and any relaxed outer zone
- Whether grades apply before or after coating
- Comparison standard set, or the required magnification and instrument for dimensional grades
- Bevel and edge requirements, and how chips outside the clear aperture are treated
- Sampling plan and report format, if records are required
How GIAI handles cosmetic inspection on custom optics
GIAI reviews custom optical projects against the drawing, sample, optical requirements, substrate, geometry, coating conditions and inspection criteria before defining the manufacturing route. Cosmetic requirements are part of that review: the surface-quality callout, inspection zone and acceptance method are confirmed for the specific part rather than assumed from a fixed company-wide grade, and spectral or other optical performance is verified separately according to the part specification. More detail on the quality workflow is available on the Quality Assurance page.
FAQ
Is a 60-40 surface worse than a 40-20 surface?
Under MIL-PRF-13830B, yes: 60-40 permits brighter scratches and larger digs (up to 0.40 mm) than 40-20 (up to 0.20 mm). “Worse” only matters relative to the application. 60-40 is widely used for general-purpose optics, while laser and imaging surfaces near a focus or image plane usually need tighter grades. Choosing a tighter grade than the system needs increases cost without improving performance.
Can scratch-dig be measured with a microscope?
Dig diameters and dimensional grades, such as ISO 10110-7 area grades or ANSI OP1.002 letter grades, can be measured under magnification. A MIL-style scratch visibility number cannot: it is assigned by visual comparison with calibrated standards under specified lighting, and scratch width does not reliably predict visibility.
Do defects outside the clear aperture matter?
Surface quality grades normally apply inside the clear aperture, and the area outside it is often given a relaxed requirement or none. Edge chips still matter: they must not intrude into the clear aperture, and large chips can weaken the part or shed particles. If the outer zone affects stray light or mounting, state its requirement on the drawing.
Does a good scratch-dig grade guarantee a high laser damage threshold?
No. Scratch-dig limits visible surface imperfections, while laser-induced damage threshold depends on the coating design, substrate, cleanliness, subsurface damage and test conditions. A tight cosmetic grade reduces potential initiation sites, but LIDT must be specified and tested on its own terms.
Why does a part pass at the supplier and fail at incoming inspection?
The usual causes are different lighting or comparison standards, contamination picked up in transit, damage during packaging or handling, or a callout that both sides interpreted differently. Agreeing on the standard, method, zone and comparison set before production removes most of these disputes.
Send your surface-quality requirement for review
For a custom lens, window, filter, mirror or prism, send the drawing or sample together with the surface-quality callout for each surface, the standard and method, clear aperture, coating requirements, wavelength range and expected quantity. Our engineers will review the inspection criteria with the rest of the specification — contact GIAI or read about our custom optics process.
References
- MIL-PRF-13830B — U.S. military performance specification covering the manufacture and inspection of optical components, including scratch-dig surface quality.
- ISO 10110-7:2017, Optics and photonics — Preparation of drawings for optical elements and systems — Part 7: Surface imperfections.
- ISO 14997:2017, Optics and photonics — Test methods for surface imperfections of optical elements.
- ISO/TR 14997-2:2022, Test methods for surface imperfections of optical elements — Part 2: Machine vision.
- ANSI/OEOSC OP1.002 — U.S. standard practice for specifying and inspecting surface imperfections on optical elements and assemblies.