Technical Resources
How to Specify a Custom Optical Coating
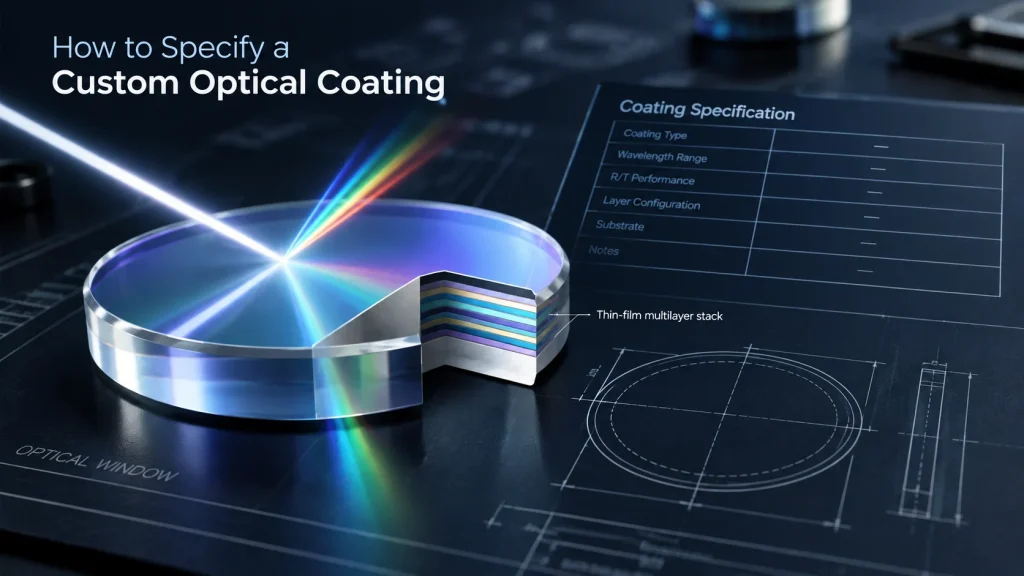
To specify a custom optical coating, describe the performance you need rather than the layer stack: the coating function and coated surface, the spectral bands with numeric limits (average or absolute), the angle of incidence, cone angle and polarization, the substrate and coated area, the durability and laser conditions, and how the result will be measured and accepted. A coating requirement is complete only when a supplier could measure every line of it.
Most coating problems found at incoming inspection are not deposition failures. They are specification failures: a reflectance limit with no wavelength band, a filter edge specified at normal incidence for a part used at 45°, or a transmission target that the uncoated back surface makes physically impossible. The steps below follow the order in which a coating engineer reviews a request, so each line you write answers a question that would otherwise come back as a clarification or, worse, get resolved by assumption.
What a custom optical coating specification must define
A usable specification has six blocks. Leaving any of them open does not make the coating cheaper; it transfers the decision to whoever designs the coating, and their default may not match your system.
| Specification block | What to state | Why it matters | Typical omission |
|---|---|---|---|
| Function and surface | Coating type (AR, HR, bandpass, edge, dichroic, beamsplitter, protective metal), which surface(s), and what the other surface carries | Defines the design family and the measurement geometry | “Both sides AR” when one side carries a filter |
| Spectral performance | Wavelength bands, R/T/OD limits, average vs absolute, edge position and slope definitions | The core of the design and of acceptance | “R < 0.5%” with no band or statistic |
| Illumination conditions | AOI or AOI range, cone half-angle, polarization state | Interference coatings shift and split with angle | Spectrum specified only at 0° |
| Substrate and geometry | Material, thickness, surface shape, coated area vs clear aperture, flatness after coating | Index, curvature and stress all change the result | Coated area left undefined on curved or thin parts |
| Environment and laser use | Temperature range, humidity, cleaning, abrasion, adhesion tests; laser wavelength, pulse width, repetition rate | Determines material choice and process route | “Durable” or “high power” with no test or numbers |
| Verification and acceptance | Measurement on part or witness, instrument conditions, sampling, cosmetic standard, data to deliver | Turns the requirement into a pass/fail decision | No agreed test method, so pass/fail is disputed later |
Step 1: Start from the system function, not the layer design
Write what the surface must do in the system: transmit 420–680 nm with minimal ghosting, reflect a 1064 nm beam at 45°, pass 850 nm and reject ambient light out to the detector cutoff. That is a performance specification, and it lets the coating engineer choose materials, layer count and deposition process to meet it.
A design specification, such as a list of layer materials and thicknesses, makes sense only when you must match an existing qualified coating. Even then, pair it with the spectral result you expect, because the same nominal stack deposited by a different process or on a different substrate will not produce an identical curve. For background on how layer thickness relates to wavelength, see optical thickness vs physical thickness in thin films.
State every surface explicitly. Typical entries are “S1: bandpass coating; S2: broadband AR 750–950 nm” or “S1: protected aluminum; S2: uncoated, fine ground.” Identify S1 on the drawing or with an edge mark so the coated side and the light direction cannot be confused.
Step 2: Write spectral requirements that can be measured
Bands, limits and statistics
Every spectral line needs four elements: a wavelength range, a quantity (R, T or OD), a limit, and a statistic. “Average” and “absolute” are not interchangeable. Ravg < 0.5% over 450–650 nm allows local peaks above 0.5% as long as the band average stays below it; Rabs < 0.5% over 450–650 nm (also written Rmax) requires every wavelength in the band to stay below the limit. The absolute form is usually harder to achieve, so use it where a local peak would actually hurt, such as at a laser line, and use the average form where the system integrates over the band.
For filters and edges, define the reference point. A cut-on wavelength is commonly defined at 50% of peak transmission, but some drawings use 50% absolute transmission or a 10%–90% transition width. Write which convention applies and give a tolerance. The tolerance logic for center wavelength and bandwidth is covered in optical filter spectral tolerance explained.
| Vague requirement | Measurable requirement |
|---|---|
| AR coated for visible | S1 and S2: Ravg ≤ 0.5% per surface, 420–680 nm, AOI 0–15°, unpolarized |
| High reflection at 1064 nm | Rs ≥ 99.5% and Rp ≥ 99.0% at 1064 nm, AOI 45° ± 2° |
| 850 nm bandpass, block everything else | CWL 850 nm ± tolerance, FWHM with tolerance, Tavg ≥ target over passband; OD ≥ target from 400 nm to detector cutoff, excluding passband; AOI 0°, half-cone ≤ stated value |
| Dichroic, reflect blue, pass red | Ravg over reflect band, Tavg over transmit band, 50% edge wavelength with tolerance for s, p or average polarization, AOI 45° |
Blocking and optical density
An OD requirement without a wavelength range is incomplete. The range should cover every wavelength where your source emits and your detector responds, not just the region near the passband. A silicon sensor still responds above 1000 nm, so an NIR-blocking requirement that stops at 900 nm can leave a leak the system will see. The method for setting the range is discussed in how to specify OD blocking range for a bandpass filter.
Also ask how high blocking will be verified. Very high OD values can exceed the dynamic range of a standard spectrophotometer, in which case the measured curve shows the instrument floor rather than the coating. Agree in advance whether such levels are verified by a higher-dynamic-range method, on a witness sample, or by design calculation.
Step 3: Define angle of incidence, cone angle and polarization
Interference coatings are angle-sensitive. As AOI increases, the spectral features of a multilayer coating move toward shorter wavelengths. A widely used approximation for a bandpass filter is:
λ(θ) ≈ λ0 · √(1 − (sin θ / neff)²)
where λ0 is the wavelength at normal incidence, θ the angle of incidence in air and neff the effective index of the coating design. As an illustration, an 850 nm filter with an assumed neff of 2.0 shifts by about 3.2 nm at 10° and about 7.1 nm at 15°. The real shift depends on the design, so if your system uses a range of angles, specify the full range rather than a single nominal value.
Two further conditions belong in the specification:
- Cone angle. In a converging or diverging beam, the filter sees a spread of angles at once. The result is a broadened, shifted and slightly lower passband. State the half-cone angle at the coated surface; see cone half-angle effect on interference filters.
- Polarization. At oblique incidence, s- and p-polarized light see different effective indices, so edges split and reflectance differs. A 45° dichroic or beamsplitter specification must say whether limits apply to s, p, both, or the average. See how polarization affects optical filter spectra at oblique incidence.
Step 4: Tie the coating to the substrate and part geometry
The substrate is part of the optical design. Its refractive index determines what an AR coating must match, its transmission range limits where any coating can work, and its thickness and stiffness determine how much the part bends under coating stress. Give the material grade, not only the generic name.
Define the coated area separately from the clear aperture. Edges held by tooling may be uncoated or show a transition zone, which is acceptable only if it falls outside the clear aperture. On steeply curved lenses, the deposited thickness falls off toward the edge, and the spectrum shifts with it. If edge performance matters, say where the specification applies, for example “within the central 90% of the clear aperture.”
Thick reflectors, edge filters and narrowband filters carry enough film stress to change the surface figure of a thin substrate. If you have a flatness or wavefront requirement, state whether it applies before or after coating, at which wavelength, and over which aperture. Coating both sides, choosing a thicker substrate, or relaxing the post-coat figure tolerance are trade-offs to discuss at the quotation stage, not after delivery. Related reading: how to specify a custom optical window.
Step 5: Specify environment, durability and laser exposure
Environmental and mechanical durability
“Durable coating” is not testable. Name the tests and the levels. Common references include the ISO 9211 series (Part 3 for environmental durability and Part 4 for specific test methods such as abrasion) and the older MIL-C-48497A, which defines adhesion (tape), humidity and abrasion tests for interference coatings. MIL-C-48497A is an inactive document, but its test methods remain widely quoted on drawings. If you reference it, write the specific tests you require rather than citing the whole document.
Also state the operating and storage temperature range, any exposure to condensation, salt fog or chemicals, and how the surface will be cleaned in service. Cleaning method matters: a coating that passes a cheesecloth abrasion test may still be damaged by an aggressive solvent or wiping routine. Coating hardness and process choice are compared in hard coated vs soft coated optical filters and IBS vs IAD optical coating.
For temperature-sensitive designs such as narrowband filters, include the operating temperature at which the spectral specification must hold. Spectral position can drift with temperature, so a specification met at room temperature may not be met at the system’s operating point.
Laser exposure
A laser damage threshold has meaning only with its test conditions. Provide wavelength, pulse duration, repetition rate, beam diameter at the optic, and whether operation is CW or pulsed. LIDT testing is commonly referenced to the ISO 21254 series, and results depend on the test protocol (for example 1-on-1 versus S-on-1). Specify the fluence or power density your optic actually sees, plus a safety margin you define, rather than a generic “high-power” label. The factors behind coating damage resistance are explained in what determines the laser damage threshold of a coating.
Step 6: Agree on verification and acceptance
Part or witness sample
Spectral performance is often measured on a flat witness sample coated in the same run, because lenses, prisms and thick or small parts are difficult to measure directly. A witness represents the part only if its material, index and position in the chamber are comparable. For curved or large optics, the witness may not show the thickness fall-off at the part edge. Agree whether acceptance is based on the part, on the witness, or on both, and which measurement is binding if they differ.
Measurement conditions
Write the conditions under which each specification line is measured: AOI, polarization, beam convergence, wavelength resolution and whether the measurement is single-surface or total. Commercial spectrophotometers usually measure with a converging beam of a few degrees, which can affect steep filter edges and polarizer performance.
The single-surface versus total distinction is a frequent source of disputes. Consider a glass window with an index near 1.52, AR coated on one side only. Even if the AR surface reflects only 0.5%, the uncoated back surface reflects about 4.3%, so the measured transmission of the part cannot exceed roughly 95%. A specification of “T > 99%” for that part is unachievable by any coating. Specify the AR surface by reflectance, or specify total transmission only when both surfaces are defined.
Sampling, cosmetics and documentation
- Sampling plan: state whether every part, every coating run, or a defined sample is measured spectrally.
- Cosmetic quality after coating: reference the surface imperfection standard used on the drawing, such as ISO 10110-7 or MIL-PRF-13830B, and state that it applies to the coated surface.
- Drawing notation: ISO 10110-9 defines how surface treatments and coatings are indicated on optical drawings, with functional coating requirements written in tabular form.
- Deliverables: measured curves per run or per part, data format, test certificates and any durability test records.
Over-specified verification costs money just as over-specified performance does. The cost effect of tight limits, multiple measurements and special tests is discussed in what makes optical coating expensive.
Common mistakes when specifying optical coatings
- No band or statistic on a limit. “R < 0.25%” can mean a V-coat at one line or a broadband average; the designs and prices differ widely. See V-coat vs broadband AR coating.
- Specifying at 0° for a tilted part. A 45° dichroic specified at normal incidence will not meet the system requirement.
- Ignoring polarization at oblique incidence. Unpolarized averages can hide a p-polarization leak.
- Blocking range that stops short of the detector response. The leak simply moves to the unspecified region.
- Physically inconsistent totals. Transmission plus reflection cannot exceed 100% for any surface, and an uncoated back surface sets a ceiling on part transmission.
- Tight limits everywhere. Applying the strictest value across all bands, angles and surfaces raises layer count, process time and cost without improving the system.
- No agreed test method. Without measurement conditions, the same part can pass at the supplier and fail at incoming inspection.
Example: turning a vague request into a usable coating specification
The following is an illustrative example of specification structure, not a GIAI product specification or a statement of achievable limits.
Original request: “Visible AR coating on both sides of a 25 mm window, low reflection, durable.”
Rewritten specification:
- Part: plane window, material and grade per drawing, Ø25 mm, clear aperture as drawn.
- S1 and S2: broadband AR, Ravg ≤ [value] per surface over 420–680 nm; Rabs ≤ [value] at 532 nm.
- Conditions: AOI 0–15°, unpolarized; specification applies within the clear aperture.
- Durability: adhesion tape test and moderate abrasion test per the method named on the drawing; operating temperature range [range].
- Verification: single-surface reflectance measured on a witness of the same material coated in the same run, near-normal incidence; measured curve supplied per coating run.
- Cosmetics: surface quality per drawing, applied after coating.
Each bracketed value comes from your optical budget. The structure ensures that the coating engineer, the inspector and your incoming QC are reading the same requirement.
What to send with a custom optical coating RFQ
- Drawing or sketch with surfaces labeled, or a reference sample.
- Coating function per surface and the spectral requirements written as in Step 2.
- AOI or AOI range, cone half-angle and polarization.
- Substrate material and grade, dimensions, coated area and clear aperture; post-coating flatness requirement if any.
- Source spectrum and detector type when blocking is involved.
- Operating environment, cleaning method and required durability tests.
- Laser parameters if the optic is in a laser path.
- Verification method, sampling plan and data deliverables.
- Quantity, prototype or production status, and target schedule.
If a requirement is still open, say so and give the system constraint behind it. A stated range such as “the AOI may be 0–20°, to be fixed after mechanical design” is more useful to a coating engineer than a guessed number.
GIAI Photonics supports custom coated optics, including AR, reflective, filter, dichroic and beamsplitter coatings on filters, lenses, windows, mirrors and prisms. GIAI reviews custom optical projects against the drawing, sample, optical requirements, substrate, geometry, coating conditions and inspection criteria before defining the manufacturing route, and acceptance methods are agreed per project. See our quality assurance and custom optics process pages for how requirements are reviewed and verified.
FAQ
Should I specify the layer design or the coating performance?
Specify performance in most cases: bands, limits, angles, polarization and environment. The coating engineer then chooses materials and layer structure to meet them with the available process. Give a layer design only when you need to replicate an already qualified coating, and still state the expected spectral result, because the same nominal stack can produce a different curve on another substrate or process.
What is the difference between Ravg and Rabs in a coating specification?
Ravg limits the average reflectance across a band, so individual wavelengths may exceed the value. Rabs, often written Rmax, limits reflectance at every wavelength in the band. Use the absolute form where a local peak matters, such as at a laser line or a narrow illumination band, and the average form where the system integrates over a broad spectrum.
Do I need to specify the angle of incidence for an AR coating?
Yes, whenever the part is used away from normal incidence or over an angular range. AR performance changes with angle and becomes polarization-dependent at oblique incidence. For small angles the change may be minor, but for wide-angle imaging or tilted windows the design must account for it, and the specification should state the full AOI range and whether limits apply to s, p or average polarization.
Is a witness sample measurement enough to accept coated parts?
Often it is, provided the witness uses the same material, is coated in the same run and is positioned representatively. It is less reliable for strongly curved, large or thick parts, where coating thickness and measurement geometry differ from the witness. Agree before production whether acceptance is based on the witness, on the part, or both, and which result governs.
How do I specify coating durability?
Name specific tests and conditions instead of a general term. Typical requirements include an adhesion tape test, humidity exposure, abrasion resistance, temperature cycling and resistance to the cleaning solvents used in service. Reference a recognized method, such as the ISO 9211 series or MIL-C-48497A test methods, and state which tests apply to production parts and which only to qualification.
Have a coating requirement to review?
Send the drawing or sample with the spectral bands, AOI and polarization, substrate, coated area, environment, laser conditions and inspection criteria to susan@giaitech.com, or use the contact page. Our engineers will review the specification before quoting.
References
- ISO 9211-1:2024, Optics and photonics — Optical coatings — Part 1: Vocabulary.
- ISO 9211-3, Optics and photonics — Optical coatings — Part 3: Environmental durability; ISO 9211-4, Part 4: Specific test methods.
- ISO 10110-9:2016, Optics and photonics — Preparation of drawings for optical elements and systems — Part 9: Surface treatment and coating.
- ISO 21254 series, Lasers and laser-related equipment — Test methods for laser-induced damage threshold.
- MIL-C-48497A, Coating, single or multilayer, interference: durability requirements for (inactive).
- Laser Focus World, “Measurement considerations when specifying optical coatings.”